I walked into Bill’s Auto Parts in 1990 to help my in-laws with a business they had just bought. I didn’t know anything about auto recycling, but I knew a mess when I saw one. Cleaning out the old and organizing for the new taught me something I have carried for 35 years: your inventory is worth more than you think, and most of that value is lost to habit.
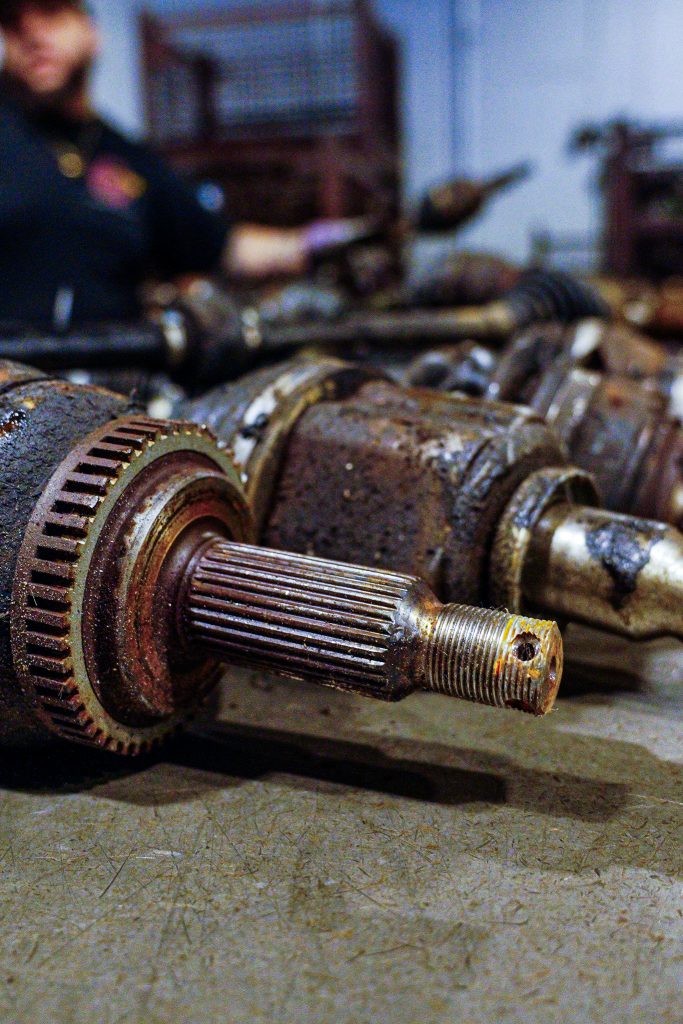
Nowhere is that more true than with auto cores. For a lot of recyclers, cores are an afterthought. A box in a dark corner. A short list of parts someone pulls when there’s time. That approach leaves real money on the table every month.
This guide lays out what I call Auto Core Competency: the people, processes, and financial tracking that turn cores from a side job into a steady revenue stream. Whether you run a full-service operation, a self-service yard, a scrap processor, or a hybrid, the principles are the same.
Cores are not junk. Cores are merchandise.
What is Auto Core Competency?
Oxford defines a core competency as “a defining capability or advantage that distinguishes an enterprise from its competitors.” Applied to our industry, Auto Core Competency is the blend of people, processes, and infrastructure focused on cores and commodities (non-parts revenue) that delivers significant bottom-line results and becomes a competitive asset.
Put simply: you already paid for the vehicle. A core program is how you collect on the parts your customers will never buy.
Why cores deserve a seat at the table
Cores are the bonds of your “partfolio”
Most of us invest in vehicles for their parts. But not every part sells, and the cost of goods on end-of-life vehicles, fees included, has never been higher. Every vehicle has to return as much value as possible for the least labor.
Look at your business as a portfolio of revenue streams. Catalytic converters and scrap have swung wildly over the years, riding precious metal prices and steel markets. Cores are different. Pricing and demand are among the most consistent of any by-product we produce. They may not have the highest yield, but done right they deliver steady income month after month, like the CDs and bonds in a financial portfolio.
You can’t budget volatility. You can budget a core box that ships like clockwork.
Where your cores actually go
Everyone knows the 3 Rs: Reduce, Reuse, Recycle. The circular economy has a fourth: Remanufacturing. Remanufacturers return used parts to like-new or better-than-new condition through a controlled, repeatable industrial process. That conserves materials, cuts energy use and waste, and keeps quality parts on the shelves of national retailers instead of cheap knockoffs that force everyone’s prices down.
With over 8,000 recyclers in the US and Canada, remanufacturers can’t buy from each one directly. Core suppliers like RAS bridge that gap, using the VIN and part ID numbers to value your inventory accurately and get the right cores to the right rebuilder. Understanding that chain is why quality matters: the part you pack today is headed for a retail shelf.
People: the backbone of a core program
There is no higher priority than having the right people in the right positions. Many family businesses avoid titles for fear of hearing “that’s not my job.” In my experience, that resistance is a management issue, not a people issue. Build a great team and they’ll walk through fire for you.
The problem with no titles is that everyone is expected to do everything, so no one gets to be great at what they’re great at. Professionalizing the core function means defining the work, setting measurable expectations, and deciding how you will measure success.
Your inventory person is now your most important core asset
In the past, the parts puller or dismantler made or broke a core program. Today it’s the person entering your inventory. They have the data: quantity on hand (QOH), days on hand (DOH), and request and sales history. With that information they can decide which cores are worth pulling before anyone picks up a wrench.
My rule: I would rather spend a few minutes of brain energy sifting through data than burn scarce labor pulling parts with low or zero value.
Roles to consider
- Core and Commodity Manager. Oversees all non-parts revenue: cores, wire, converters, aluminum wheels, recalled parts, and other non-ferrous material. Evaluates programs for profitability and manages the technicians. Fits larger operations.
- Auto Core Technician. Removes and QC-checks cores, recalled airbags, and commodities, and stages and packs core boxes. Especially valuable for self-service and scrap processors, where staff often lack mechanical backgrounds and tooling.
- Vehicle Dismantler. In full-service shops, cores belong in the dismantler’s written job description, not as an afterthought to the drivetrain pull.
Whether cores are 100% of someone’s job or one line in it, write it down. If it’s left open-ended, the results will reflect the effort.
Process: identify, recover, QC, pack
Every successful core program comes back to four basics: Identification, Recovery, QC, and Packing. Get these right and the money follows.
1. Identification: cherry-pick, don’t strip
Old-school thinking says pull a standard list (alternators, starters, A/C compressors, maybe calipers) from every vehicle and hope for a payday. We don’t strip every part off a car to put on the shelf, so why do it with cores?
I once worked with a small yard pulling a four-part list from every vehicle. When one of those part types lost its core value, 25% of everything they pulled was worth nothing. Once the data showed them what was happening, they switched to cherry-picking from a longer list that included steering, advanced electronics, and brakes. Their next core box came in at double the value.
New-school thinking reverses the process. Run the VIN, see the value up front, and spend your labor on the cores that pay. Printed lists go stale before they come out of the printer. Live data doesn’t.
2. Recovery: fit cores into the workflow you already have
Pulling cores shouldn’t mean a separate trip to every vehicle. There are five natural contact points in any operation where cores can be identified or recovered with minimal extra labor: vehicle/core inventory, time of dismantle, core returns, loose parts inventory, and pre-crush.
Read more: Cores Are a Contact Sport: Five Contact Points for Cores in Your Workflow
When a vehicle is already on the lift for an engine sale, the technician, tools, and data are all in place. Pulling the alternator, starter, and steering pump at that moment isn’t extra work. It’s incremental time.
3. Quality control: know what can be rebuilt
Chasing the highest-dollar cores is pointless if the part is wrong or damaged. Most deductions come from a short list of repeat mistakes: aftermarket or previously rebuilt parts, locked-up pulleys, broken housings and plugs, excessive rust, and missing part or stock numbers.
Read more: The 7 Deadly Sins of Cores
4. Packing: give your cores some love
When I ask recyclers where their cores are, I’m usually sent to the darkest, dampest corner of the building. Based on what we see at RAS, our best estimate is that 20 to 25% of products arrive damaged from poor packing. On a $2,400 box, that can mean $600 in deductions.
- Set up a well-lit staging area with a rack next to your gaylord box.
- Stage cores on the rack, then pack by weight: heavy-duty on the bottom, then medium, then light.
- Put flat cardboard between layers.
- Bubble wrap delicate electronics (instrument clusters, infotainment units, ECMs) and box them separately.
- Never throw cores into the box.
- Keep rack and pinions, especially EPS units, out from under heavier cores. They’re often your most valuable cores, and they pack differently.
Read more: How to Pack a Core Box
Financial: it’s not what you make, it’s what you keep
If you can’t see cores on your P&L, you can’t manage them. Many recyclers I’ve consulted with don’t review a monthly P&L at all, usually because theirs has been patched for years and is unreadable.
Give non-parts revenue its own lines
Sit down with your accountant and review your chart of accounts. Break out cores, converters, scrap, commodities, and recalls, then group them so you can see non-parts revenue as a percentage of your total. Most recyclers are surprised by how much it adds up to, and once you see it, you start managing it.
Track the numbers that matter
Your core supplier’s settlement statement holds everything you need. Pull these numbers into a simple spreadsheet for every shipment:
| Metric | What it tells you |
|---|---|
| Core turn rate | How often you ship. Monthly is better than quarterly. Consistency lets you budget. |
| Paid % | What you were paid versus what you invoiced. Think of it like a school grade. |
| Variance $ and % | Dollars left on the table, and why. |
| Number of parts | Compare against parts invoiced. Uninvoiced extras are a red flag. |
| Average $ per part | The root of the analysis. Low averages can cost more to ship than they return. |
I’m an average guy. In my experience, boxes of 100 to 200 cores typically average $12 to $18 per part. Averages under about $8 per part rarely make sense once you count labor and freight. To raise your average, target higher-value cores and drop the low-value ones.
Read more: Reading Your Core Settlement Statement
Reward quality, not just quantity
Incentives are great, but they have to be managed. Pay for quantity alone and you’ll get full boxes with low yields. Tie incentives to average value per part and the percentage of invoiced parts actually paid, and everyone wins: the recycler, the employee, the core buyer, the remanufacturer, and the planet.
Where to start this month
- Name one person responsible for cores, and write it into their job description.
- Have your inventory person run a VIN-based core search on every incoming vehicle.
- Move your core staging area somewhere bright, and add a rack.
- Retrain your team on the 7 Deadly Sins of Cores.
- Pick one or two core vendors and commit to a regular shipping rhythm.
- Add non-parts revenue to your P&L and track average $ per part on every box.
These changes won’t happen overnight. But a culture of change leads to better priorities, better decisions, a better workplace for your team, and higher profits. Let’s professionalize auto cores together.
Talk to the RAS cores team about your core program.